



I. INTRODUCTION
Welding residual stresses are primarily owing to the differences in temperature distribution in the weld and parent metal during heating and cooling cycles (Withers and Bhadeshia, Reference Withers and Bhadeshia2001). These thermally induced stresses can exceed yield and cause strain misfit on cooling. Residual stresses can lead to fracture, reduced fatigue life, and stress corrosion cracking (Webster and Wimpory, Reference Webster and Wimpory2001). Residual stress can also lead to hydrogen cracking and distortion, which are significant problems in shipbuilding; the cost of correcting weld distortion in shipbuilding may be up to 30% of the fabrication costs (Andritsos and Perez-Prat, Reference Andritsos and Perez-Prat2000). Welding distortion is affected by many factors, including component design, welding sequence, and heat input, with the most important factor being the level of residual stress. Residual stresses may cause hydrogen cracking of welds in the presence of trapped hydrogen and a susceptible microstructure, often defined as a microstructure with a hardness value of more than 350 HV (API Standard 1104, 2005; CSA-Z662, 2007). Microstructures with high hardness values are caused by the same high temperatures which cause residual stresses, with the addition of fast cooling rates. Hydrogen content can be controlled by electrode choice and welding procedure.
Neutron diffraction (ND) can be used to obtain residual stresses non-destructively with high spatial resolution of ≤1 mm to a depth of many millimetres below the weld surface (up to 50 mm for steel). ND been successfully applied to evaluate residual stresses in many welded components (Law et al., Reference Law, Kirstein and Luzin2010; Paradowska et al., Reference Paradowska, Price, Finlayson, Lienert and Ibrahim2010a, Reference Paradowska, Price, Finlayson, Rogge, Donaberger, Blevins and Ibrahim2010b; Assuncao et al., Reference Assuncao, Yapp, Suder, Ganguly, Williams and Paradowska2011; Law and Luzin, Reference Law and Luzin2011; Suder et al., Reference Suder, Ganguly, Williams, Paradowska and Colegrove2011).
The pulsed tandem gas metal arc welding (PT-GMAW) process promises to: (1) deliver high deposition rates; (2) perform out-of-position welding; and (3) achieve low levels of weld distortion (Yudobidroto et al., Reference Yudobidroto, Hermans and Richardson2006). Residual stresses have not been previously measured in PT-GMAW welds, and this experiment aims to investigate, using ND, the hardness and residual stress profiles of welds made by PT-GMAW.
II. EXPERIMENTAL
A. Samples
The samples were DH36 steel plates 4.5 mm thick × 200 mm wide × 300 mm long, and HSLA65 steel plates of 8 × 150 × 285 mm3. Welds were made along the whole length, in full penetration mode. Both samples were made by PT-GMAW, which used a ceramic backing and a Fronius PT-GMAW system in pulse–pulse mode, a shielding gas of 16.5% CO2, 1.5% O2, and 82% Ar flowing at 30 l min−1, a torch angle of 10° (push), a wire feed speed of 12–16 m min−1, and a travel speed of 750 mm min−1.
B. Hardness testing
Hardness testing was performed across the weld with a Leco micro hardness testing machine with an indentation mass of 1 kg. The HSLA65 weld is harder than the DH36 weld in every zone (Figure 1). In both the materials, the heat-affected zone is hardest, followed by the weld, and then the parent material, with the differences being greater in the HSLA65 material. No hardness values are above 350 HV, which is where hydrogen cracking is likely to occur.
(Color online) Hardness traverse of DH36 and HSLA65 welds.

C. Neutron residual stress measurements
Knowing the neutron wavelength (λ) and the Bragg scattering angle (θ), and the inter-planar spacing (d) can be calculated via the Bragg equation. If the inter-planar spacing (d 0) of an unstressed sample is also known (Figure 2), the elastic strain in the scattering vector direction can be calculated via
 $$\varepsilon=\displaystyle{d \over {d_0 }} - 1$$
(Color online) Peak shift between unstressed (a) and stressed (b) gauge volumes, indicating a strain of 867 microstrain.
When the strains in a number of directions are known the full stress field can be calculated (Hutchings and Krawitz, Reference Hutchings and Krawitz1992; Hutchings et al., Reference Hutchings, Withers, Holden and Lorentzen2005). The simplest solution is when the strains are measured in the same direction as the three principal stresses, then
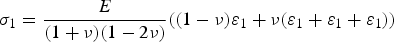 $$\sigma _1=\displaystyle{E \over {\lpar 1+\nu \rpar \lpar 1 - 2\nu \rpar }}\lpar \lpar 1 - \nu \rpar \varepsilon _1+\nu \lpar \varepsilon _1+\varepsilon _1+\varepsilon _1 \rpar \rpar $$
The example shown in Figure 2 shows a peak shift of 0.101°2θ, which indicates a strain of 867 microstrain. In a uniaxial stress state, this would be equivalent to a stress of 173 MPa, but the actual value in a component depends on the other two strains.
Through-thickness scans were performed on the weld and parent material (Figure 3) in three directions orthogonal to the plate axes, which were assumed to be the same as the principal stress directions. The longitudinal stress is aligned with the weld direction, the transverse stress is cross-weld, and the normal stress is through-thickness.
(Color online) Welded sample during measurement on the Kowari instrument. The primary beam comes from the monochromator; the secondary beam is the diffracted neutrons. The measured strain direction lies between these two beams.
The residual stress measurements were performed on the Kowari strain scanning instrument at the OPAL research reactor at the Australian Nuclear Science and Technology Organisation (ANSTO). A monochromatic beam of λ = 1.672 Å was chosen, so that the Fe (211) scattering planes in the sample resulted in a scattering angle close to 90o, which reduces many possible geometric errors in measurement (Hutchings et al., Reference Hutchings, Withers, Holden and Lorentzen2005). A nominal gauge volume of 1 × 1 × 1 mm3 was used. Each sample was measured at three through-thickness positions, 1 mm below each surface and in the middle of the thickness. Since the composition and microstructure vary across the weld and parent material, stress free (d 0) lattice spacing values were made for each measurement point. To calculate the stresses from the strains, values for Young's modulus (E) of 207 GPa and Poisson's ratio (ν) of 0.3 were used for both steels.
D. Residual stress results
The residual stress maps for the welded plates are shown in Figure 4. The residual stress profiles across the weld of the plates 1 mm below the surface are shown in Figure 5. The residual stress has been compared with the minimum yield strength for each steel grade.
(Color online) Residual stress profile through-thickness of the DH36 4.5 mm plate (left) and HSLA65 8 mm plate (right). Longitudinal stresses (a), transverse stress (b), and normal stresses (c).
(Color online) Residual stress profile: (a) 1 mm below the surface across the DH36 4.5 mm welded plate, and (b) the HSLA65 8 mm welded plate.
In both welds, the residual stress in the along-weld direction (longitudinal) was highest. The normal direction residual stress for DH36 was compressive or close to zero across the weld, and transverse residual stresses were highest in the vicinity of the weld. The residual stresses in the DH36 material were lower, and also had a lower gradient between the parent and weld, both of which will reduce distortion. For the HSLA65 weld, transverse residual stresses were higher on either side of the weld. Normal direction residual stresses (through-thickness) were compressive in the vicinity of the weld, and close to zero outside of the weld.
E. Comparison of hardness and residual stress results
The hardness of the DH36 shows a slow decline from the weld toward the parent metal (Figure 1), and the residual stress profile for this steel shows the same trend (Figure 5). The highest residual stresses and hardness were both found in the HSLA65 weld, reflecting the higher yield strength of the weld material. Although the highest hardness values are below the 350 HV limit for hydrogen cracking, the coincidence of these with the position of highest residual stresses demonstrates the potential for hydrogen cracking if the welding procedure is not adhered to.
III. CONCLUSION
Detailed residual stress and hardness distributions were presented for welds made by PT-GMAW on DH36 and HSLA65 steels. In both materials, the highest stresses were found in the weld material and lie in the weld direction. These were balanced by lesser compressive residual stresses in the parent material. The cross-weld stresses are self-balancing and are highest in the crown of the weld. Transverse residual stresses were found to be highest in the middle thickness of the plate in both welds. The HSLA 65 welded plate had the highest residual stresses. The position of highest hardness values corresponds to the position of highest residual stress. The DH36 material's residual stress distribution will lead to less distortion.



