I. INTRODUCTION
Improving the depth of penetration capability is one of the primary goals of the welding processes adopted in industries. In the recent past, activated flux assisted welding has been one of the promising, notable techniques for joining various metal combinations, with a focus on maximizing the depth of penetration. In general, the fluxes such as sulphides, halides, and/or oxides which are dissolved in the solvents, such as carbinol, ethanol, or acetone. This flux is precoated on the plates to be joined using a paint brush or dispenser. Researchers addressed that the arc constriction and marangoni convection are the underlying mechanisms, contributing for the improved depth of penetration. Although a deep weld penetration could be obtained from activated flux tungsten inert gas (A-TIG) welding process, the oxidization of the tungsten electrode often occurs simultaneously. It was proven that the penetration capability of A-TIG welding had been increased to 200–300% compared to conventional TIG welding.
Similarly, several researchers have addressed the use of laser welding for joining versatile materials. Some of the typical advantages include the narrow beads with lesser or nil heat affected zone (HAZ), lower distortion, improved mechanical properties, and higher productivity. However, the use of low kW capacity laser welding machine for joining high thickness materials is cumbersome task. Kuo et al. Reference Kuo, Sun and Pan1 performed the flux assisted laser welding of mild steel, austenitic, and duplex stainless steels. The authors used a 3 kW CO2 laser welding equipment for carrying out the studies. According to the authors, more than one penetration mechanism is involved in the laser welding with the use of flux. The investigations showed that the activating flux not only improved the penetration depth through arcing characteristics in the TIG and plasma welding processes but also that it was beneficial for the laser welding technique itself in the conduction mode. Sun et al. Reference Sun, Song and Zhang2 carried out laser welding of Mg-AZ31B alloy using three different fluxes namely SiO2, TiO2, and Cr2O3. The authors reported that for the same power, the weld penetration decreases with increasing welding speed both with and without flux. The authors used 500 W Nd:YAG laser welding equipment for this alloy. As indicated by Ma et al., Reference Ma, Hu, Hu, Shen and Wang3 laser welding with activating flux is a very complex heat transfer and fluid flow process.
Super-austenitic stainless steel, AISI 904L, is one of the emerging stainless steel grade, which has unique applications in marine, defense, and nuclear industries. Due to the presence of higher amounts of molybdenum, chromium, nickel, nitrogen, these grades of stainless steel exhibit better weldability and higher corrosion resistance than the conventional austenitic stainless steel grades. A complete austenitic structure would be existing throughout the transformation from liquid to solid for this typical stainless steel due to the presence of higher amounts of Ni and N. Although these materials exhibit good weldability, one of the major drawbacks associated with the welding of AISI 904L is the segregation of Mo. Researchers addressed the Mo segregation could be reduced on using overalloyed filler metals or by using faster cooling rates in the welding process.
Devendranath Ramkumar et al. Reference Devendranath Ramkumar, Narasimha Varma, Chaitanya, Choudhary, Arivazhagan and Narayanan4 observed the existence of Mo-rich phase during the A-TIG welding of AISI 904L. The authors further claimed that although the Mo-rich phases were present, they were found to be in lower amounts while using A-TIG welding compared to the conventional TIG welding process. In a study, Zambon et al. Reference Zambon, Ferro and Bonollo5 used CO2 laser welding for joining 3 mm thick sheet of AISI 904L and investigated the microstructure, tensile properties, and the residual stresses of the welded joints. The authors observed the formation of an imperceptible HAZ. Sathiya et al. Reference Sathiya, Mishra and Shanmugarajan6 carried out CO2 laser–gas metal arc welding hybrid welding process for joining 5 mm thick AISI 904L plates using super-austenitic solid filler metal. The authors investigated the effect of shielding gases on the bead morphology, mechanical properties of AISI 904L laser hybrid weldments. Further, the authors noticed that the use of 50% He + 50% Ar resulted in better tensile properties, whereas the shielding gas mixture containing 50% He + 45% Ar + 5% O2 welded joints exhibited higher impact toughness values.
From the open literature, it is opined that limited efforts have been addressed on the flux assisted laser welding hitherto. This study addresses the possibility of utilizing a low power Nd:YAG laser welding machine with the aid of oxide flux to obtain a complete penetration. Although some studies have been reported on the flux assisted laser welding process for joining metals, the assessment of metallurgical and mechanical properties of AISI 904L super-austenitic stainless steel has not been carried out so far. The outcomes of the present study will be highly beneficial to the industries using AISI 904L.
II. EXPERIMENTAL PROCEDURE
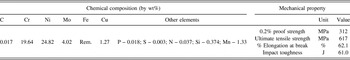
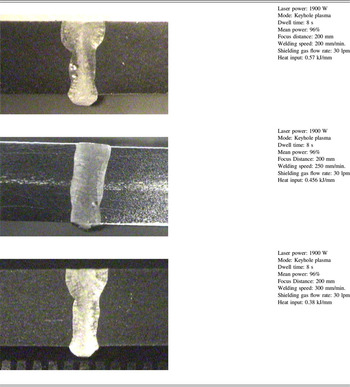
The chemical composition of the as-received AISI 904L has been tested using dry spectroscopic methods and is represented in Table I. The bead on trials was carried out on the 904L plates whose dimensions were 200 mm × 60 mm × 5 mm. A 2 kW Nd:YAG laser welding equipment (Model: JK2003SM) was used for the welding trials. The diameter of the laser beam is 300 µm and the focus distance was maintained at 200 mm. The laser welding was conducted using keyhole mode. As described by Kuo et al., Reference Kuo, Sun and Pan1 a keyhole would be formed when laser welding energy density exceeds a critical value. The high energy density in laser welding would transfer the heat from the laser source to the material and not to a point on the surface, but to a line extending through the material thickness. Hence, the welds would be deeper and narrower. Commercially available pure SiO2 flux was used in the study, which was mixed with carbinol, a carrier solvent, to obtain paint like consistency. A uniform coating was applied on the plates using the paint brush. The bead on trial welds was carried out using different welding speeds 200, 250, and 300 mm/min as the researchers reported that lower welding speeds result in better penetration (Table II). Incomplete penetration was noticed on increasing the welding speed above 300 mm/min. The bead on test trial coupons was subjected to x-ray radiography nondestructive testing (NDT) technique to determine for porosity defects. The studies revealed the occurrence of porosities for the speeds 200 and 250 mm/min. The porosities of dimensions 25 and 30 µm for 200 mm/min and 1.7 µm for 250 mm/min were observed. Zambon et al. Reference Zambon, Ferro and Bonollo5 also observed similar types of porosities while CO2 laser welding of 3 mm thick sheets of AISI 904L. While evaluating the beads, welded with a speed of 300 mm/min as per EN 462/1 standard, porosities of dimension greater than 150 µm were not detected.
Chemical composition and mechanical properties of base metal, AISI 904L.

Macrostructure of the beads obtained from SiO2 flux assisted laser welding of AISI 904L.

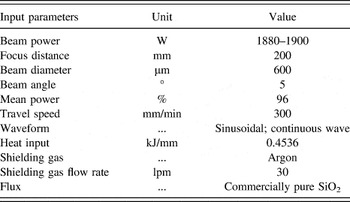
Based on the bead trial results, the welding speed of 300 mm/min was chosen for the butt welding of AISI 904L plates. Before welding, the plates were cleaned with sand papers followed by cleaning with acetone. A 15 mm wide flux coating was applied throughout the length of the plates, keeping joint line at the center. The flux quantity applied on the plate was 5–6 mg/cm2, as the coating thickness has significant impact on the depth of penetration as reported by Ahmadi and Ebrahimi. Reference Ahmadi and Ebrahimi7 The butt joints of AISI 904L were obtained using the flux assisted laser welding in a 2 kW capacity Nd:YAG laser machine. The parameters used in the flux assisted laser welding are given in Table III.
Process parameters used for flux assisted laser welding.

The same NDT technique was again followed for the butt joints of AISI 904L. Ensued to the results, the coupons were cut from the weldment using wire-cut electrical discharge machining process. The coupons were fabricated according to the standards prescribed by ASTM. Optical Microscopy and scanning electron microscopy (SEM) analyses were carried out on the cross-sectional coupons of dimensions 28 mm × 10 mm × 5 mm. Standard metallographic procedures were adopted and electrolytic etching (10% oxalic acid; 6 V DC supply; 1.6 A/cm2) was used to reveal the microstructure of the laser weldment. Hardness measurements were carried out on the cross-sectional coupons both in the longitudinal as well as in the transverse sections of the weldments using Vickers microhardness tester. A standard load of 500 gf was applied for a dwell time of 10 s and the readings were made at the regular intervals of 0.25 mm. Tensile studies were carried out on the weldments prepared as per the ASTM E8/8M standard using Instron Universal Testing machine. The cross-head velocity was maintained as 2 mm/min to induce a slow strain rate of 3.3 × 10⁻⁴ s−1. Charpy V-notch impact test was conducted on the coupons fabricated in accordance with ASTM E23:12C standard. Three trials in each test were conducted to ensure the repeatability of the results. Further, the fractured samples are investigated to assess the mode of fracture using SEM analysis.
III. RESULTS AND DISCUSSION
A. Effect of flux on the weld penetration and porosity
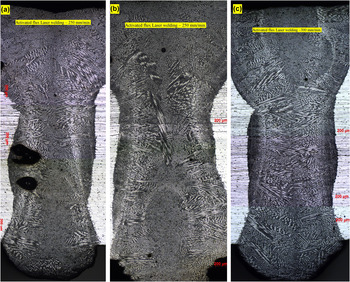
Despite the use of lower welding speed and a lower kW capacity laser welding machine, the use of SiO2 flux and adequate dwell time for the keyhole formation during laser welding resulted in full penetration. As pointed out by Qin et al., Reference Qin, Wang and Zou8 the absorption of laser energy by the oxides is more than that by fluorides which was indicated by comparing the weld width for full penetration weld. According to Sun et al., Reference Sun, Song and Zhang2 the SiO2 flux had better absorptivity for YAG laser. X-ray radiography and macrostructure studies divulged the presence of porosities while using the welding speeds 200 and 250 mm/min [Figs. 1(a) and 1(b)]; whereas operating with 300 mm/min speed resulted in complete penetration along with the absence of gas porosities [Fig. 1(c)] while performing the bead on studies. With the same power, lowering the welding speeds improved the weld penetration. Similar results have been reported by Sun et al. Reference Sun, Song and Zhang2 The authors further added the heat input should be nominal and not to be increased beyond the critical value. This would be due to the fact that the increase in heat input shall vaporize the flux coat, thereby the energy reaching the surface would be shielded, making it harder for the laser energy to be absorbed by the weld pool, and decreasing the penetration. It is evident from the current study that a nominal amount of heat input is provided to establish the beads with complete penetration. This could be attributed to the surface tension and arc constriction effect. In conventional arc welding process such as TIG, the surface tension would be higher at the edges of the weld pool than at the center under the arc. Hence, the flow of the molten metal would be outwards and results in shallow and broader beads. However, with the use of oxide flux, the surface tension would be higher at the center than at the edges, forcing the fluid flow inwards and causing the deeper penetration. This is well in agreement with Qin et al. Reference Qin, Wang and Zou8 According to the authors, the Marangoni convection induced by surface tension difference drives the molten metal flow from the edges to the center of the weld pool. This pattern of fluid flow brings the energy to the interior of the molten pool, resulting in a deeper penetration.
Micrograph of the flux assisted Nd:YAG laser welded AISI 904L at (a) 200 mm/min, (b) 250 mm/min, and (c) 300 mm/min welding speed.

While using the welding speed of 300 mm/min, for the butt welding using SiO2 flux assisted laser process, the formation of gas pore was witnessed closer to the root portion of the weld zone. The pore size is much smaller of ≤1 µm compared to the works carried out by other researchers. Moreover, the porosity was observed at the location where the keyhole emerged and the rest of the weldment was free from any porosities which was confirmed by both x-ray radiography and dye penetrant NDT inspection methods. However, further studies are needed to investigate the effect of activating flux on the penetration and porosity. Matsunawa et al. Reference Matsunawa, Kim, Seto, Mizutani and Katayama9 investigated the keyhole dynamics and melting during laser welding. According to the authors, the instability of the keyhole would cause the formation of porosity or cavities in the weld metal. Further, the authors observed that the keyhole opening quickly and closes after laser power termination. This in turn suggested that the sudden collapse of the keyhole led to the entrapment of metal vapor and shielding gas. Therefore, it would be necessary to stabilize the keyhole during cooling to prevent collapse. This could be also due to the presence of some or all the bubbles in the weld pool, mainly metallic vapor and shielding gas and sometimes captivated air, could be trapped by the instability and collapse of the keyhole during welding, causing porosity in the welds. Similar studies have been reported elsewhere. Reference Kaplan, Mizutani, Katayama and Matsunawa10,Reference Norman, Drazhner and Prangnell11 The content of the trapped bubbles would depend on many factors such as, nature of shielding gas, vapor pressure of the metal, viscosity of the molten metal, and dynamics of the keyhole during the welding process. Similarly, the floatability of bubbles could be affected by the type of waveform (continuous or pulsed), surface tension of the molten metal, direction of the molten metal flow as described by several researchers. Reference Kaplan, Mizutani, Katayama and Matsunawa10,Reference Kuo12–Reference Seto, Katayama and Matsunawa16 It is well understood that the porosity in the laser welds shall be attributed to any of these factors. Also, the study attested that the complete penetration of 5 mm thick plates could be achievable using SiO2 flux and also by utilizing low power (2 kW) continuous wave laser welding process.
B. Interfacial and weld microstructure
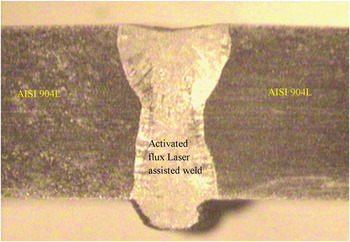
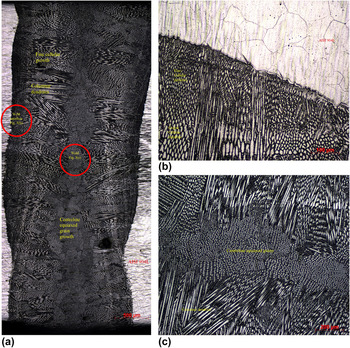
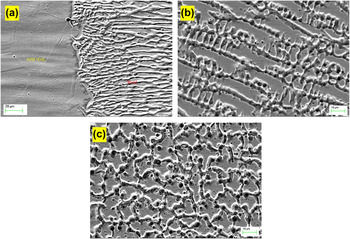
Metallurgical and mechanical characterization studies were carried out on the porosity free zone of the weldment as similar type of study had been reported by Zambon et al. Reference Zambon, Ferro and Bonollo5 during the CO2 laser welding of AISI 904L. The macrostructure and the microstructures of the flux assisted laser welded joint are shown in Figs. 2 and 3. Interfacial microstructure showed the absence of HAZ and/or any other formation of secondary phases which could be due to the low heat input as well as presence of Cu alloying element in AISI 904L and also the use of copper back plate which effectively dissipated the heat. Microstructure of the fusion zone was observed to have various grain growths, such as columnar dendrite, cellular dendrites, and equiaxed grains. Both the formation of elongated and fine cellular along with the columnar dendrites was observed at the interface of AISI 904L; whereas the formation of uniform, finer equiaxed grains was witnessed along the centerline of the fusion zone. The higher magnification images of microstructure at the interface and the fusion zone are shown in Figs. 4(a) and 4(b). As reported by Norman et al., Reference Norman, Drazhner and Prangnell11 the formation of a fine equiaxed dendritic microstructure in the center of autogenous welds shall be due to the development of an undercooled liquid ahead of the moving solid–liquid interface, which provides the correct thermal conditions for the nucleation and growth of new grains. Moreover, as described in the earlier section, the surface tension gradient would be greatest at the center than at the edges. Therefore, as the molten fluid flows inwards due to the surface tension gradient, the solidification rate would be greater at the center of the weld pool than at the edges. The finer grain structure at the centerline of the fusion zone could be seen in the high energy beam welds or arc welds made with low welding speeds. Similar observations are reported elsewhere. Reference Lampman17 Although several mechanisms, such as grain detachment, dendrite fragmentation, and heterogeneous nucleation for nucleating equiaxed grains near the weld centerline have been proposed, the recent experiments divulged that the dominant mechanism for equiaxed growth could be heterogeneous nucleation. Reference David and Vitek18
Macrograph of the flux assisted Nd:YAG laser welded AISI 904L.

(a) Microstructure of flux assisted laser welded AISI 904L. (b) Interface microstructure of flux assisted laser welded AISI 904L. (c) Weld microstructure of flux assisted laser welded AISI 904L.

(a) SEM photograph at the weld interface of AISI 904L. (b) SEM showing fusion zone microstructure showing columnar dendrites at the weld interface and (c) equiaxed grains at the centerline of the weld zone.

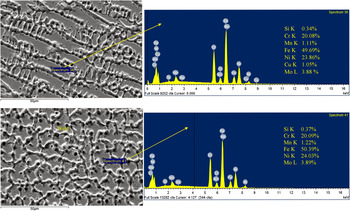
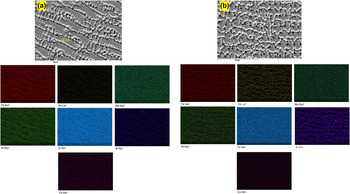
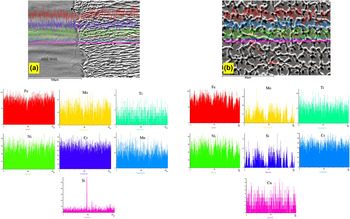
SEM/energy dispersive x-ray analysis (EDAX) point analysis at the fusion zone adjacent to weld interface and the middle is shown in Figs. 5(a) and 5(b). The matrix of both the fusion zones was found enriched with elements containing Fe, Ni, Cr, and Mo. It could be understood well that fully austenitic structure would be prevailing in the fusion zone of the flux assisted laser welding. Similarly, the elemental mapping carried out at the fusion zone signifies that the grain body was enriched with higher amounts of Ni and Mo apart from Fe and Cr [Figs. 6(a) and 6(b)]. However, excessive Mo segregation was not observed between the matrix and the grain body. This clearly elucidated the Mo segregation could be reduced on using faster cooling rates. Also the elemental line mapping analysis was carried out at the weld interface and in the centerline of the fusion zone to investigate the elemental movement across the zones. It is inferred from Fig. 7(a), the elemental migration from AISI 904L to the fusion zone was very meager; whereas a closer observation on Fig. 7(b) clearly portrayed the migration of Mo, which was found to be more at the grain body which appeared as white shiny facets.
SEM/EDAX point analysis at the fusion zone of flux assisted laser weldments of AISI 904L.

(a) Elemental mapping analysis at the fusion zone adjacent to the interface of AISI 904L. (b) Elemental mapping analysis at the centerline of the fusion zone of AISI 904L.

(a) Line mapping analysis at the interface of AISI 904L. (b) Line mapping analysis at the fusion zone of AISI 904L.

C. Mechanical characterization of the weldment
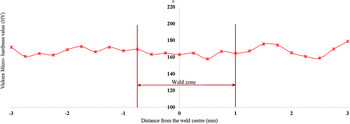
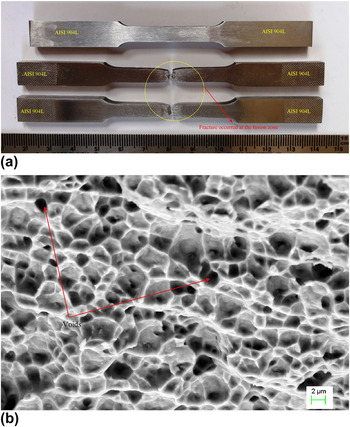
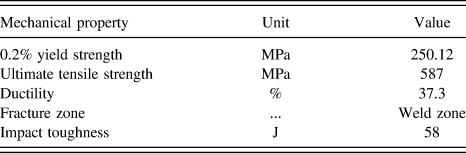
Hardness measurements were carried out on the cross-sectioned coupons across their entire length as well as at the centerline of the fusion zone. The hardness profile of the activated flux assisted laser welded AISI 904L is shown in Figs. 8(a) and 8(b). It is evident from the studies that there was not much difference in the observed hardness values of the parent metal and the fusion zone. The average hardness of the parent metal and the fusion zone was found to be 168 and 164 HV, respectively. The average hardness at the centerline of the fusion zone was found to be 162 HV. On the basis of the microstructure and hardness measurements, it is clearly understood that there was no much elemental segregation or the formation of any new secondary phases at the fusion zone. It was inferred from the tensile studies that the fracture occurred at the fusion zone of the weldment for all the trials [Fig. 9(a)]. However, the tensile strength and ductility of the flux assisted laser weldment of AISI 904L were found to be 587 MPa and 37.3%, respectively, which were greater than that of the earlier works of the authors [MSEA paper]. The joint efficiency [defined as (UTS weld joint)/(UTS base metal) × 100] of the flux assisted weldment laser welded AISI 904L was established to be 95.14%. The strength slightly degraded due to the band of fine, equiaxed grains present in the centerline of the fusion zone. As reported by several researchers, this could be attributed to the relatively high level of constitutional supercooling during the solidification and faster cooling rates, which would impart the reduction in strength. Reference Lippold and Kotecki19 Also, the hardness data are in agreement with the tensile properties. SEM fractograph clearly divulged the presence of microvoids along with the dimpled facets coalesced to undergo ductile fracture [Fig. 9(b)].
Hardness trend of the flux assisted laser welds of AISI 904L.

(a) Tensile photographs of activated flux assisted laser welded AISI 904L showing the fracture at the fusion zone. (b) SEM fractograph showing the tensile tested AISI 904L flux assisted laser weldment.

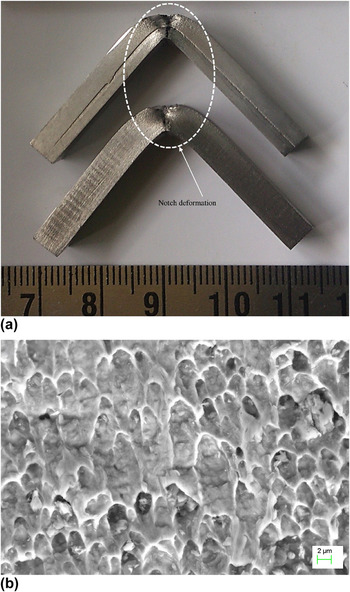
Impact studies divulged that the average impact toughness of the weldments was found to be 58 J, which is closer to the parent metal (61 J). It is inferred from the charpy v-notch studies that the weldments had undergone notch deformation and did not completely rupture [Fig. 10(a)]. This indicated that the weldments have adequate ability to store impact energy. This study attested an improvement in toughness while using the flux assisted laser welding process. It could be attributed to the reduction or almost nil amount of oxides present in the fusion zone compared to the earlier works of the authors. Reference Devendranath Ramkumar, Narasimha Varma, Chaitanya, Choudhary, Arivazhagan and Narayanan4 It is well understood from the various research works that the use of oxide flux improves the weld penetration and deteriorates the weld toughness. SEM fractograph vividly showed the presence of scarce voids along with dome shaped cleavage facets, which attested for mixed mode of fracture [Fig. 10(b)]. Table IV shows the average tensile and impact properties of SiO2 flux assisted laser weldments of AISI 904L.
(a) Impact test photographs of activated flux assisted laser welded AISI 904L showing v-notch deformation. (b) SEM fractograph showing the impact tested AISI 904L flux assisted laser weldment.

Cumulative tensile and impact properties of activated flux laser welded AISI 904L.

As a whole, this study addressed the use of SiO2 flux for joining the AISI 904L plates using a 2 kW Nd:YAG laser machine. Due to the faster cooling rates developed in the high energy processes, such as EB and laser welding process, the grain growth will be uniform. This study successfully addresses the welding of 5 mm thick plates by coupling the use of flux as well as the laser welding. Although several research works have been attempted in the flux assisted laser welding, very few attempts have been reported on high thickness materials. One of the problems attested from the current study was the formation of a typical gas pore which was observed in the beginning of the weldment i.e., the location at which the keyhole plasma emerged. Hence, the appropriate use of shielding gas, varying the dwell time in providing the plasma as well as beam oscillations may eradicate such problems. The mechanical and metallurgical characterization was accomplished on the flux assisted laser weldment. The tensile strength of the weldments has been improved as compared to the earlier works of the authors. Reference Devendranath Ramkumar, Narasimha Varma, Chaitanya, Choudhary, Arivazhagan and Narayanan4 A detailed structure–property relationship of the weldments addressed in this study would be highly beneficial to the end users demanding the use of AISI 904L.
IV. CONCLUSIONS
The following conclusions could be drawn from the present investigation.
-
(1) Successful joints of AISI 904L with 5 mm thick plate could be accomplished using flux assisted low power (2 kW) laser welding process.
-
(2) Multidirectional grain growth containing cellular and columnar dendrites along with the presence of centerline fine equiaxed grains was observed.
-
(3) A small porosity was observed at the specific location (near keyhole) of the weldment not throughout the entire length of the weldment.
-
(4) Tensile strength of the flux assisted laser welded AISI 904L was reported to be 587 MPa. The impoverishment of tensile strength could be attributed to the centerline equiaxed grains.
-
(5) Impact toughness of the weldment was closer to the parent metal, which would be due to the absence of oxides in the fusion zone.
ACKNOWLEDGMENT
The authors sincerely thank the Department of Science and Technology (DST) - Science & Engineering Research Board (SERB) for funding this project under the Young Scientist Scheme (Project No. YSS/2014/000706). The authors also sincerely thank the DST for funding the laser welding machine and Instron Universal Testing facility to our University under DST-FIST scheme.