Nomenclature
- FLSC
-
flexible linear-shaped charge
- LSC
-
linear-shaped charge
- LBSSS
-
linear bellow-based stage separation system
- M
-
molecular mass of the detonating products
- MDC
-
Mild Detonating Cord
- P
-
pressure developed by detonating products
- P real
-
realistic pressure developed inside free volume of steel tubes
- PETN
-
pentaerythritol tetranitrate
- Q
-
quality factor
- R
-
universal gas constant
- SMA
-
shape-memory alloy
- SRS
-
shock response spectrum
- SSS
-
stage separation system
- T
-
detonation gas temperature
- V
-
free volume inside steel tubes
- w
-
explosive mass
1.0 Introduction
Separation mechanisms play a critical role in multistage launch vehicles, satellites and other aerospace systems where structural subsystems must disengage in a timely and controlled manner. Efficient separation is essential to mission success, ensuring that payloads are released accurately while minimising mechanical disturbances and ensuring system integrity post-event. Over the decades, a variety of separation mechanisms have been developed, broadly categorised into pyrotechnic and non-pyrotechnic systems. Pyrotechnic-based separation mechanisms, such as pyrobolts, explosive bolts and flexible linear-shaped charges (FLSCs), have traditionally been the industry standard due to their compact design, high reliability and ability to deliver rapid energy release [Reference Burnham1]. These mechanisms typically involve detonation-induced structural failure, making them suitable for quick, fail-safe separations. However, they come with inherent disadvantages, including high pyroshock, generation of debris, irreversible actuation and potential damage to nearby sensitive instruments and subsystems [Reference Ott and Folkman2]. Notably, shock levels from pyrobolt- and FLSC-based systems can exceed 10,000 g across high-frequency ranges, which poses significant qualification challenges for spacecraft components [Reference Jeyakumar and Biswas3–Reference Firsyuk, Ermakov, Tufan and Vasikov5]. Researchers have also worked on other confined detonation systems like that of Super*zip cord-based stage separation systems (SSS). Williams [Reference Williams6] examined the performance of the Super*zip cord-based separation system, which employs two MDC cords to ensure reliable initiation and mitigate notch failure. The Super*zip cord has been implemented in the Space Shuttle programme as well as the Titan IV booster separation system. Additionally, they developed a zip cord-based separation system featuring a single MDC cord, designed for use in missile applications. Bement et al. [Reference Bement, Schimmel and Louis7] investigated different failure modes in the Super*zip separation systems utilised in the Space Shuttle programme. To this end, over 300 tests were conducted to analyse the target severance mechanism and identify the most likely causes of failure. The insights gained from this rigorous analysis contributed to the design of a more reliable separation system.
In contrast, non-pyrotechnic separation mechanisms have gained increasing interest due to their reusability, lower shock and potential for multiple actuations [Reference Hwang, Kim and Choi8, Reference Lee and Han9]. These include separation nut actuators, shape memory alloy (SMA)-based release systems [Reference Lee, Son, Hwang, Kim and Kim10], pin pullers, frangible joints and electromagnetic actuators [Reference Ermakov, Tufan and Firsyuk11]. Despite their low-shock advantage, non-pyro mechanisms often suffer from increased system complexity, power consumption, slower response times and potential failure modes in extreme environments. Among the emerging alternatives is the use of pneumatic- or gas-based separation mechanisms, which operate by releasing pressurised gases to generate mechanical motion for separation [Reference Chen, Zhu, Chen, Zhao and Yin12]. Pneumatic systems offer relatively low shock and the potential for clean separation, but face limitations in terms of system mass, storage of compressed gases, sealing challenges and reduced performance in vacuum environments. While many of these alternatives have demonstrated operational success, they often suffer from increased mass, reduced reliability in cryogenic environments, or complexity in actuation mechanisms.
SSS are integral to the performance and success of multi-stage launch vehicles and long-range missiles. These systems facilitate the detachment of depleted stages during flight, allowing the active stages to proceed with reduced mass and improved propulsion efficiency. A properly functioning SSS enhances the overall mission reliability by optimising the vehicle’s structural configuration and ensuring efficient transitions through different atmospheric regimes, from lift-off to high-altitude cruise and eventual orbital insertion. A typical SSS comprises actuation mechanisms, hold-and-release systems and separation impulse devices. The actuation mechanisms, often electro-explosive devices such as pyro cartridges or electric initiators, trigger the separation sequence, which cuts the section into two parts. Hold-and-release systems are mechanical or pyrotechnic structures that keep the stages securely joined until separation is commanded. Mechanical systems may use clamps, diaphragms, or point-release mechanisms, whereas pyrotechnic systems include explosive bolts or linear-shaped charges (LSC) to rapidly sever connections. Separation impulse is generally achieved using preloaded springs, retro-rockets, ullage motors or open interstage configurations. These components collectively ensure a clean break between stages and prevent recontact or instability during separation.
The selection of an SSS architecture depends on mission-specific requirements such as structural stiffness, shock tolerance and mass constraints. FLSC-based systems are commonly used in lower-stage separations where high bending moments are encountered. These systems, while structurally robust, generate considerable pyro shock, necessitating that sensitive avionics and electronics be placed at a safe distance – typically more than 800 mm – from the separation plane. Additionally, FLSC-based systems require retro motors to generate separation thrust, which significantly increases overall system weight. These motors are typically fabricated from steel and are arranged symmetrically in even numbers (2, 4 or 8) to ensure balanced separation forces. Pyrobolt-based systems, which are suitable for moderate structural requirements, also rely on retro motors and are slightly less intense in shock generation compared to FLSC systems. In contrast, Marman band separation systems are favoured in payload and upper-stage applications where minimal shock is critical. These systems use mechanical bands and compressed springs to achieve clean separation and are relatively lightweight. Despite their proven reliability, traditional systems carry the burden of high pyro shock and significant added mass due to the use of separation impulse devices like retro or ullage motors. Typically, these motors contribute 40 to 100 kg of weight, and their synchronised activation within a narrow time window (approximately 10 milliseconds) is crucial to avoid rotational instabilities or collision between the stages. While the hold-and-release mechanism itself may be light, the overall weight of the SSS becomes substantial due to these impulse-generating subsystems.
To address these limitations, the present study introduces a novel linear bellow-based stage separation system (LBSSS) that eliminates the need for retro motors and offers a low-shock, debris-free separation mechanism. This concept leverages the concept of shock and debris confinement through mechanical encapsulation. The system being investigated in the present work integrates both pyrotechnic and mechanical elements in a novel configuration designed to drastically reduce pyroshock transmission. This hybrid approach is particularly valuable in applications where low shock transmission, positive separation velocity, compact size and high reliability are simultaneously required. This system has been extensively used for the upper stage payload fairing separation system. In a detailed examination, Whalley [Reference Whalley13] delineated the payload fairing separation system utilised in the STARS II launch vehicle. This system employs a circumferential separation mechanism facilitated by FLSC for the payload shroud, along with thrusting linear explosive rail joints that achieve vertical separation, oriented perpendicularly to the vehicle’s trajectory. The paper thoroughly investigates the underlying explosive principles and presents findings from full-scale developmental tests conducted in this domain. Furthermore, Cheng et al. [Reference Cheng14] conducted a comprehensive study on the dynamics of heat shield separation, based on a linear bellow separation system, in both Titan and Delta launch vehicles. His research involved the formulation of an analytical model that meticulously accounts for various factors, including the quantity of gas produced by the explosive, the failure mechanisms of rivets and the dynamic thrusting interactions of the heat shield during separation.
The core principle of the proposed bellow-based stage separation system is to utilise a flexible, high-strength rubber bellow assembly that envelops the explosive detonation zone and absorbs the resultant energy in a controlled manner. The system comprises two primary structural elements: the piston rail and the cylinder rail, which are initially joined by mechanical fasteners such as rivets. Sandwiched between these two components is a skewed rubber bellow, which is designed to be compliant enough to expand upon pressurisation, yet robust enough to withstand the thermal and dynamic loading from the detonation gases.
Embedded within a central channel running along the assembly is a MDC, enclosed within steel tubes with vent holes. The role of these MDCs as a medium for gas generation has been discussed in the works of Kumar et al. [Reference Kumar, Chakraborty, Srinivasan, Srikanth and Srinath15]. These tubes serve multiple functions: they attenuate the initial detonation shock, confine solid fragments and metallic debris and regulate the outflow of gases through engineered vent holes. The venting design ensures that only high-pressure gases are allowed to exit the steel tube and enter the bellow chamber, which subsequently inflates and drives the separation action by shearing the riveted connection between the piston and cylinder rails. The deployment sequence begins with the initiation of a single detonator, which activates the MDC. The explosive gases produced expand rapidly within the confinement of the steel tubes, venting into the bellow chamber. The resultant pressurisation of the bellow leads to its rapid expansion, applying sufficient force to separate the two structural members. This action is achieved with significantly reduced shock transmission, owing to the layered containment of detonation effects by both the steel housing and the rubber bellow.
Figure 1 shows a detail of the working principle of the bellow-based separation mechanism. Compared to open detonation systems like FLSCs, the bellow-based separation mechanism offers several distinct advantages:
-
• Reduced pyroshock levels due to shock confinement and attenuation
-
• Minimal debris ejection, enhancing the system’s cleanliness and safety
-
• Positive and symmetric separation motion due to bellow inflation
-
• Simplified initiation architecture using a single initiator
-
• Compact and modular design, allowing integration in space-constrained vehicle interfaces
While the LBSSS weighs slightly more than the FLSC-based hold-and-release system alone, it offsets the need for heavy retro motors, resulting in a net reduction in system mass. Furthermore, the system is highly configurable; the separation impulse can be tailored by adjusting the charge quantity of the MDC and modifying the structural strength of the rubber bellow. This technology holds promise for both circumferential stage separations and longitudinal applications such as payload fairing deployment [Reference Suresh and Sivan16], offering a cleaner, lighter, and more shock-tolerant alternative to traditional pyrotechnic systems.
Principle of bellow-based separation mechanism.

The present research paper outlines the detailed development, material selection, design iterations and experimental validation of this novel bellow-based low-shock stage separation system. The focus is to demonstrate its feasibility as a reliable alternative to conventional high-shock explosive systems, particularly for future launch vehicle applications prioritising low dynamic loads and clean separation dynamics.
2.0 Test rig and instrumentation plan
To evaluate the functional performance of the developed bellow-based low-shock stage separation system, a dedicated ground test setup was designed and fabricated to simulate the operational conditions of the piston–cylinder separation mechanism. The objective of this setup was to mimic the dynamic separation behaviour of the mechanism, including the shearing of structural fasteners (rivets), expansion of the rubber bellow under high-pressure gas loading and to capture the critical parameters such as pressure buildup, shock transmission and separation dynamics.
2.1. Test rig description
The core structure of the test rig comprised two flat interface plates, each rigidly attached to the simulated piston-rail and cylinder-rail subassemblies. These plates formed the base platforms for assembling the actual separation mechanism. At the centre of the assembly, the rubber bellow and the perforated steel guide tubes housing the MDC were mounted. The thickness of the rubber bellows is 3 mm, composed of multiple layers of 0.5 mm thick neoprene rubber and nylon fabric. This construction imparts both flexibility and strength to the bellows. The bellow was arranged in a skewed configuration to ensure uniform expansion dynamics upon detonation. The perforated steel tube assembly comprises of two concentric steel tubes. The inner tube features a row of 3 mm diameter holes, drilled along the length of the tube. The outer tube contains a row of 3 mm diameter holes, which is also drilled along the length, specifically oriented towards the free volume of the rubber bellow to facilitate efficient gas filling. This assembly functions as a shock attenuator and operates as a filter, permitting only gases to enter the rubber bellow. Additionally, all holes were meticulously deburred to prevent any risk of puncturing the rubber bellow. The piston and cylinder sections were then joined using high-shear rivets, which were dimensioned based on the expected separation force generated by the internal pressure. The weight of the simulated blocks associated with the piston and cylinder is 5 kg. The total weight of the cylinder assembly is 9.7 kg, which includes the rubber bellow, steel tubes, cylinder interface, detonator end, pressure transducer end, two sets of guide rails and the simulated block. In contrast, the piston assembly weighs 6.9 kg, comprising the piston interface, two sets of guide rails and the simulated block.
The entire assembled mechanism was mounted on precision low-friction linear guide rails, allowing for unrestricted lateral motion of the piston-rail and cylinder-rail subassemblies post-actuation. This ensured an accurate representation of the in-flight relative motion between stages during actual launch vehicle separation events. Both ends of the test rig were rigidly enclosed by steel bulkhead covers, providing mechanical support and containment for internal gases and ensuring safe venting.
2.2. Initiation and instrumentation layout
To initiate the MDC, a pyrotechnic detonator was connected at one end of the steel tube assembly. This initiator was triggered remotely, and its signal was synchronised with the data acquisition system and high-speed camera for precise time correlation. The opposite end of the steel tube was connected to a piezo-resistive pressure transducer, which was used to monitor the pressure developed within the rubber bellow chamber following detonation. Two pressure transducers, PT1 & PT2, were used for the test. PT1 measures the pressure generated inside the steel tube while PT2 measure the pressure developed inside the rubber bellow. This configuration enabled real-time assessment of the explosive-driven gas pressure dynamics. The sampling rate of the pressure transducers is set at 10,000 samples per second.
In order to characterise the pyroshock signature of the mechanism, two tri-axial piezoelectric shock accelerometers were mounted on simulated mass blocks attached to both the piston-rail and cylinder-rail plates. The accelerometers were oriented to capture:
-
• Axial acceleration (along the length of the MDC)
-
• Perpendicular acceleration (normal to the interface plane, representing shock transmitted through the mounting structure)
-
• Tangential acceleration (along the expected direction of panel separation)
These sensors were selected for their high-frequency response and broad dynamic range, ensuring fidelity in capturing fast-transient shock pulses typically associated with pyrotechnic events. The sampling rate of the shock accelerometers is 50,000 samples per second.
Additionally, a high-speed video camera system was used to capture the entire sequence of operation visually. The video capture was triggered in synchronisation with the detonation signal to analyse the temporal delay between command initiation and physical separation, as well as to measure the separation velocity of the plates. The schematic of the test rig is shown in Fig. 2.
Schematic with instrumentation details of the flat plate separation test.

2.3. Test conditions and parameters measured
Two test configurations were executed to study the performance of the separation system under varying explosive loads:
Test 1: MDC with charge density of 5 g/m
Test 2: MDC with reduced charge density of 3 g/m
These tests were performed to examine the mechanism’s behaviour across a range of explosive energy inputs, with a specific focus on shock attenuation capability and pressure response. The critical performance parameters monitored during the tests included:
-
• Physical health and structural integrity of all components post-test
-
• Internal pressure measurements within both the steel tube and the rubber bellow chamber
-
• Panel separation velocity, based on high-speed video frame analysis
-
• Actuation delay, defined as the time lag between the initiation command and full mechanical separation
The developed test rig, with its integrated instrumentation and containment features, provided a controlled environment for assessing the repeatability, safety and dynamic response of the bellow-based stage separation system under simulated real-world conditions. Figure 3 shows the test article assembled on the test rig. Coloured markings with regular intervals were used to determine the speed of separation from the high-speed video.
Flat plate test article.

2.4. Design calculations and pressure estimation
To estimate the pressure generated during the actuation of the bellow-based separation mechanism, a chemical equilibrium analysis was carried out based on the thermodynamic properties of the explosive used in the MDC. The explosive material considered for the analysis is pentaerythritol tetranitrate (PETN), which is commonly used in MDCs due to its high detonation velocity and stable performance characteristics. For the baseline configuration, an MDC with a core load density of 5 g/m was selected.
Given a total MDC length of 500 mm, the explosive mass (w) involved in the detonation is calculated to be:
 \begin{align}\,\textrm{w} = 0.5\,\textrm{m} \times 5\,\textrm{g/m} = 2.5\,\textrm{g} \end{align}
The initial free volume (V) available within the steel tube and rubber bellow assembly prior to detonation was estimated as 36.75 cc, or V = 36.75 × 10⁻⁶ m3.
Using the ideal gas law (PV = nRT), and considering the following thermodynamic parameters:
-
• Detonation gas temperature, T = 3100 K
-
• Average molecular weight of detonation products, M = 25.63 g/mol (based on literature values)
-
• Universal gas constant, R = 8.314 J/mol.K
The peak pressure generated under ideal conditions is calculated as:
 \begin{align}\,\textrm{P} = (\textrm{wRT})/(\textrm{MV}) = (2.5 \times 8.314 \times 3100)/(25.63 \times 36.75 \times 10 -6) \approx 68.4\,\textrm{MPa} \end{align}
This value represents the theoretical maximum pressure in the confined chamber assuming complete detonation, no heat loss and ideal gas behaviour. However, in practical conditions, factors such as incomplete combustion, heat losses to surrounding materials and real gas effects contribute to a reduction in the effective pressure. Based on experimental experience and literature, a 30% reduction from the ideal value is considered to account for these non-idealities. Hence, the expected pressure inside the steel containment tube during the test is approximately:
 \begin{align}\,\textrm{P}_{\textrm{real}} = 70\% \times 68.4 = 47.8\,\textrm{MPa}\; \textrm{(478 bar pressure)} \end{align}
For the second test configuration, an MDC with a core load density of 3 g/m was used, resulting in a total explosive mass of w = 0.5 × 3 = 1.5 g.
Following the same analytical approach, the corresponding ideal pressure is:
 \begin{align} \textrm{P} = (1.5 \times 8.314 \times 3100)/(25.63 \times 36.75 \times 10^{-6}) \approx 41.04\,\textrm{MPa} \end{align}
Considering the same 30% loss due to real-world effects, the realistic pressure is estimated as:
 \begin{align} \textrm{P}_{\textrm{real}} = 0.7 \times 41.04 \approx 28.7\,\textrm{MPa (287 bar pressure)} \end{align}
These calculations provided a preliminary estimation of the gas pressures acting on the internal surfaces of the mechanism and were used to guide the material selection, bellow design and structural reinforcement of the containment tube. They also serve as a baseline for interpreting the test results and validating the functional performance of the system under two distinct charge mass conditions.
3.0 Post-test results and observations
Following the detonation and separation event for both the tests, a thorough inspection and data review were conducted to evaluate the structural, functional and instrumentation performance of the bellow-based stage separation system. The key findings from the test are summarised as follows.
3.1. Rivet shearing and structural separation
The separation mechanism performed in both tests as intended, with all rivets experiencing shearing under the action of internal gas pressurisation from the MDC detonation. Notably, all rivets sheared cleanly at the piston–cylinder interface, demonstrating consistent stress concentration and failure at the designed shear plane. In addition, all formed rivets remained attached, and no rivet debris was observed, confirming the debris-free nature of the mechanism and the success of the confined separation approach.
3.2. Visual and material observations
-
• No blackening and soot deposition were prominently observed on the piston panel, consistent with the design methodology.
-
• No structural cracks or deformation were observed on either panel, nor were there signs of thermal degradation.
-
• The rubber bellow was completely intact with no evidence of fragment ejection, supporting the system’s debris mitigation capability.
These post-test findings confirm that the bellow-based stage separation system demonstrates effective functional performance, controlled panel separation, and with no debris ejection, fulfilling the key design objectives. Post-test condition of the separation test is shown in Fig. 4.
Condition of the test article after the separation test.

3.3. Panel recovery and motion dynamics
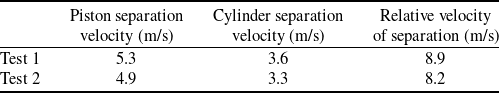
Both the piston and cylinder panels for both tests were successfully recovered from the fixture, demonstrating a clean and symmetric lateral separation. The impact-resistant blocks, serving as terminal stoppers and shock absorbers, effectively mitigated the post-separation impact energy, preventing panel over-travel and damage. The time-resolved imagery data acquired from the high-speed camera, triggered by the start signal, were analysed to evaluate the dynamic response during the separation event. Figure 5 illustrates high-speed video recorded during the first test at 1000 frames per second. At zero-time, initiation occurs upon issuing an electrical command to the detonator. This detonator activates the 5 g/m MDC, resulting in a pressure increase within the bellows, leading to their expansion. At 12 ms, the internal pressure surpasses the shear strength of the aluminum rivets, causing all the rivets to physically shear. During this interval, the explosive energy also propels both the piston and the cylinder, leveraging the available stroke length to create a thrusting separation system. As time progresses to 30 ms and 60 ms, the distance between the piston and cylinder increases. It is evident that the piston velocity exceeds that of the cylinder, attributed to the lower mass of the piston (6.9 kg). In comparison, the cylinder is heavier (9.7 kg) due to the inclusion of both steel end connectors and the pressure transducer. At 129 ms, the piston travels 680 mm and engages the stopper, with a calculated velocity of 5.3 m/s. By 189 ms, the cylinder has also travelled 680 mm to reach its stopper, with a calculated velocity of 3.6 m/s. Utilising high-speed video analysis, as described, the separation velocities were determined for both tests and documented in Table 1.
Events captured with high-speed camera during the separation test.

These values indicate rapid and effective separation with sufficient kinetic energy imparted to the panels, confirming the mechanism’s capability to generate required thrust under confined detonation.
3.4. Bellow and containment tube behaviour
The rubber bellow was totally intact after the tests, and the bellow successfully demonstrated the following characteristics:
-
• Confined the initial gas surge long enough to drive the rivet shearing.
-
• Prevented gas leakage that could reduce separation effectiveness.
-
• Absorbed shock effectively, evident from the readings of the shock sensors.
-
• The perforated steel tubes, as well as their vent holes, remained intact, confirming their robustness and effectiveness in confining solid detonation debris and regulating gas flow into the bellow chamber. The end connectors, pressure ports and sensor housings were found to be physically intact and structurally undamaged. The data from the pressure transducer (PT) were studied, and the following observations were made.
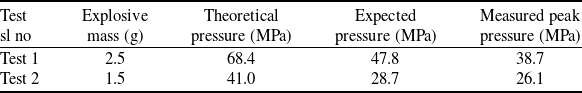
In Test 1, the MDC used had a charge density of 5 g/m, resulting in a total explosive mass of 2.5 g. The maximum peak pressure recorded in the containment tube was 394 ksc (39.4 MPa). In Test 2, the charge density was reduced to 3 g/m, corresponding to an explosive mass of 1.5 g, and the peak measured pressure was 265.9 ksc (26.6 MPa). This observed reduction in peak pressure from Test 1 to Test 2 directly correlates with the decrease in explosive mass. Specifically, the charge mass in Test 2 was 60% of that used in Test 1, and the peak pressure was found to be approximately 67.5% of the Test 1 value. This proportional relationship between charge mass and pressure generation supports the theoretical assumption of ideal detonation behaviour under confined conditions. Figure 6 shows the pressure-time history recorded inside the perforated steel tubes, where the MDC was enclosed. A comparison with the theoretical pressure estimations, accounting for a 30% loss due to real-world inefficiencies, yields the following pressure results (as tabulated in Table 2).
Panel separation velocity measured from the test

Pressure inside the steel tube (PT1) holding the explosive cord.

The measured pressures show good agreement with the theoretical predictions, especially in Test 2, where the deviation is minimal, indicating a well-confined and controlled detonation event. The pressure data from the rubber bellow, as shown in Fig. 7, displays a significant amount of high-frequency noise and spiking, particularly during Test 1. This response is attributed to limitations in the sampling rate of the data acquisition system used in the initial test. The lower sampling frequency was insufficient to accurately resolve the steep pressure gradients and rapid transients occurring within the bellow chamber immediately following detonation. As a result, the signal appears discontinuous and exhibits aliasing effects. Recognising this deficiency, the sampling rate was substantially increased for Test 2, leading to a marked improvement in signal quality, with better resolution of the pressure waveform and reduced noise artifacts. Although the peak pressure values inside the bellow remain difficult to quantify precisely due to the residual spikes, the improved time resolution allowed for better correlation of bellow inflation dynamics with panel separation motion.
3.5. Shock analysis of the separating medium
During the execution of Test 1 and Test 2, shock sensors were strategically placed at both the piston and cylinder interfaces to capture the transient dynamic response arising from the detonation of the MDC. The shock data was subsequently processed to extract the SRS, which provides a frequency-domain representation of acceleration magnitudes and is a standard metric for quantifying pyroshock environments. Figures 8 and 9 illustrates the time-domain acceleration plots, while Fig. 10 presents the corresponding SRS with a quality factor (Q) of 10 for Test 1. Q is a dimensionless parameter that is inversely related to the damping ratio (ζ), described by the equation Q = 1/(2ζ) in SRS characterisation. In the context of pyroshock quantification within aerospace applications, a damping ratio of 5% is typically assumed, resulting in Q as 10, which indicates moderate damping [Reference Lee, Chia and Kong4]. Similarly, plots of shock levels for Test 2 are shown in Figs. 11 and 12 and SRS with Q = 10 is plotted in Fig. 13.
Comparison of theoretical and experimentally obtained pressure

Pressure measured inside the rubber bellow (PT2) for two tests.

Shock levels measured on the cylinder interface for Test 1.

Shock levels measured on the piston interface for Test 1.

Shock response spectrum for the separation Test 1.

Shock levels measured on the cylinder interface for Test 2.

Shock levels measured on the piston interface for Test 2.

Shock response spectrum for the separation Test 2.

A detailed comparison of the recorded data reveals the following observations:
-
• The peak shock amplitudes recorded in Test 2 are significantly lower than those observed in Test 1. This reduction in shock level is directly correlated with the reduction in explosive charge mass used in Test 2 (1.5 g) compared to Test 1 (2.5 g), corresponding to 60% of the charge mass.
-
• This reduction in charge mass yielded peak SRS magnitudes approximately 65–70% lower than those recorded in Test 1. These findings are consistent with the pressure measurements and ideal gas law-based predictions discussed in earlier sections, where the measured peak pressure in Test 2 (265.9 ksc) was 67.5% of that in Test 1 (394 ksc).
A distinct observation from the test data is the difference in shock levels at the piston and cylinder interfaces. The piston interface, having relatively lower structural mass, exhibits higher shock amplitudes. This is attributed to its lower inertia, which allows the high-frequency content from the explosive detonation to be transmitted with minimal attenuation. Conversely, the cylinder interface, being more massive and structurally rigid, demonstrates significantly lower shock levels. The increased mass acts as a passive damping medium, effectively absorbing and dissipating high-frequency vibrational energy generated during the separation. This phenomenon is in line with classical shock propagation theory, wherein interfaces with higher impedance (mass and stiffness) tend to filter out higher frequency shock components, thereby reducing the overall shock transmissibility.
The SRS plots derived from both tests offer additional insights (as shown in Fig. 14). The Test 1 spectrum shows broader bandwidth and higher peak acceleration levels, with noticeable excitation in the 2–10 kHz frequency range, typical of explosive-driven separations. The Test 2 spectrum, while maintaining similar frequency content, shows attenuated peaks across the entire frequency domain, validating the intended design modification of lowering the explosive charge mass to mitigate shock loading.
Comparison of SRS of sensors recording maximum shock in the two tests.

3.6. Implications for structural design
The observed variation in shock levels across configurations and interfaces highlights the importance of mass distribution and explosive control in separation system design. The findings suggest that by tailoring explosive loading and strategically designing the geometry and mass distribution at the structural interfaces, it is possible to significantly mitigate shock transmission to sensitive components, thereby enhancing overall system reliability.
4.0 Conclusion
The present study aimed to develop and experimentally validate a novel low-shock, bellow-based stage separation mechanism as an alternative to conventional explosive-based separation systems. The experimental work, carried out through a specially designed test rig simulating piston-cylinder separation via rivet shear, has successfully demonstrated the functionality and effectiveness of the proposed system. MDC is housed within perforated steel tubes, successfully initiated the separation sequence by generating sufficient internal pressure to shear all rivets at the piston–cylinder interface, thereby confirming the mechanism’s ability to achieve positive and reliable structural separation. The rubber bellow remained structurally intact throughout the test. Two tests were conducted using 5 g/m and 3 g/m MDCs within the same experimental setup. The measured relative separation velocity of 8.9 & 8.2 m/s indicates that the system provides sufficient impulse for effective stage separation. The observed symmetry in the separation motion further confirms the dynamic balance and structural consistency of the mechanism. The maximum pressure in rubber bellow was recorded as 38.7 and 26.1 ksc. The observed pyroshock values on the piston side were approximately 1500 g and 900 g, while the values on the cylinder side were around 2200 g and 1110 g for the 5 g/m and 3 g/m MDCs, respectively. Both tests exhibited similar trends in pyroshock and SRS profiles. This represents a marked improvement over conventional FLSC systems, which typically produce open blast effects and high pyroshock levels detrimental to sensitive onboard systems. Post-test inspection revealed that all critical structural elements, including the bellow, containment tubes, and the panel interface, retained their mechanical integrity, demonstrating the robustness of the design under dynamic loading conditions. Overall, the results establish the proposed system as a promising low-shock, debris-free and structurally robust alternative to conventional stage separation mechanisms
In conclusion, the proposed bellow-based separation mechanism has demonstrated all the critical characteristics desired in next-generation separation systems: low shock levels, zero debris generation, reliable actuation, structural integrity and operational simplicity using a single initiator. This development paves the way for the integration of such systems in future space launch vehicles, especially in stages carrying sensitive payloads or re-entry modules, where pyroshock and contamination are critical design constraints. Future work will focus on improving instrumentation fidelity, conducting full-scale qualification under varying environmental conditions, and performing comparative studies against existing separation technologies to further quantify the reduction in shock levels.
Acknowledgements
The authors gratefully acknowledge the support and guidance of the director of Advanced Systems Laboratory for providing the necessary facilities, encouragement and administrative support throughout the course of this research. His vision and leadership have been instrumental in enabling the successful completion of this work on the development of the bellow-based stage separation system.