I. INTRODUCTION
Aluminum and its alloys are widely used in various fields, such as transportation, building, electrical engineering, as well as packaging due to their valuable mechanical, electrical, and thermal properties. These applications are well accepted through the stability of oxide film on the aluminum surface spontaneously formed in air or in contact with aqueous solutions, which shifts the corrosion potential of aluminum by nearly 1 V in the positive direction. Thus, aluminum-based materials are normally recognized to have good resistance to corrosion. Such a resistance can be a great advantage for the aluminum used as constructional materials. Another attractive property of aluminum is its standard reversible potential [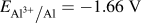 $E_{{{{\rm{Al}}^{3 + } } \mathord{\left/ {\vphantom {{{\rm{Al}}^{3 + } } {{\rm{Al}}}}} \right. \kern-\nulldelimiterspace} {{\rm{Al}}}}} = - 1.66\;{\rm{V}}$ (versus standard hydrogen electrode)], which makes aluminum used as anode material in a battery system, and sacrificial anode in cathodic protection of steel in seawater.Reference Li and Bjerrum1–Reference Bessone, Flamini and Saidman4
Recently, the use of aluminum and its alloys to produce hydrogen through reaction with water has attracted researchers due to their abundant resource on Earth, high theoretical hydrogen production (1.359 L for 1 g Al at 298 K and 1 atm) and low cost.Reference Wang, Leung, Leung and Ni5–Reference Huang, Gao, Pan, Wei, Lv, Qin and Huang7 In comparison with other hydrogen production methods such as photocatalytic method,Reference Chen, Liu, Peter and Mao8–Reference Ran, Zhang, Yu, Jaroniec and Qiao13 photoelectrocatalytic method,Reference Khaselev and Turner14,Reference Reece, Hamel, Sung, Jarvi, Esswein, Pijpers and Nocera15 electrocatalytic method,Reference Zheng, Jiao, Li, Xing, Chen, Jaroniec and Qiao16–Reference Zheng, Jiao, Jaroniec and Qiao20 thermalcatalytic method,Reference Rosen21 and biocatalytic method,Reference Chin, Chen and Chou22 Wang et al.Reference Wang, Leung and Leung23 pointed out that the cost of hydrogen from this method can be as low as US$0.2/kg-H2 if secondary aluminum is used. However, the resistance becomes the major hurdle to realizing continuous hydrogen generation through aluminum corrosion. So far, many methods have been developed to solve this problem including the addition of alloying elements with low melting points and the activation of the Al matrix by introduction of lattice strain through ball milling.Reference Fan, Xu and Sun24–Reference Mahmoodi and Alinejad28 High-pressure torsion (HPT) is one method which can consolidate powder mixture into solid state and can simultaneously introduce strain into the materials in a continuous way.Reference Valiev, Islamgaliev and Alexandrov29,Reference Valiev, Estrin, Horita, Langdon, Zehetbauer and Zhu30 However, there are few literature studies concerning the application of HPT in the hydrogen production study through reaction with water.
In the present work, Al–Sn based powders are first consolidated by HPT processing, and their hydrogen production behavior is investigated after immersing in pure water. The microstructures of the HPT-processed alloys are analyzed by x-ray diffraction (XRD), transmission electron microscopy (TEM), electron probe microanalysis (EPMA) and electron back scattered diffraction pattern (EBSP). Discussion is given for achieving an optimum condition for the hydrogen generation and for obtaining the relation with the microstructures. The mechanism why hydrogen is generated from the Al–Sn alloys in pure water is also discussed.
II. EXPERIMENTAL PROCEDURE
A. Materials preparation
Al–x wt% Sn (x = 20, 40, 60, and 80) powder mixtures were prepared by mechanical agitation using pure Al powders (99.99 wt%) with a powder size of ∼75 μm, and pure Sn powders (99.99 wt%) with a powder size of ∼38 μm. HPT was conducted at room temperature to consolidate the powder mixtures to discs with 10 mm diameter and 0.9 mm thickness under a pressure of P = 6 GPa. Shear strain, γ = 2πrN/h (r: distance from the disc center, N: number of turns, h: thickness of disc), was introduced through rotation for either N = 1, 10, or 50 turns with a rotation speed of 1 rpm. The samples processed for N = 10 were subsequently annealed at 483 K for 1 h.
B. Measurement of hydrogen generation
Hydrogen generation experiments were carried out in beakers containing 5 L pure water (resistivity is 18.2 MΩ cm) at a selected temperature of 297, 313, 323, and 333 K using a water displacement method. All the samples were ground mechanically by emery papers to be in equal surface condition before being immersed in the water. For samples conducted at room temperature, the volume of generated hydrogen was recorded every day, while for the samples conducted at higher temperatures, the hydrogen volume was recorded every 30 min during the first 2 h, then every 1 h during the subsequent 4 h and finally once a day.
C. Microstructure characterization
XRD analysis was performed using the Co Kα radiation in a scanning step of 0.01° and a scanning speed of 1°/min. LaB6 standard powders were used concurrently with the samples during XRD analysis for offsetting any possible peak shifts between measurements. For TEM, as the samples are sensitive to water, instead of common electrolytic method, a focused ion beam system was used to prepare thin foil samples from the discs at ∼4 mm away from the disc center. TEM was operated at 200 kV for microstructure observation and for recording selected-area electron diffraction (SAED) patterns. EPMA mapping was carried out at an edge part of the HPT-processed sample using a scanning beam with a current of 10 nA and a size of 1 μm. EBSP was also conducted to analyze the grain size and crystal orientation of the HPT-processed samples.
III. RESULTS
A. Hydrogen generation at room temperature
Figure 1 shows results of the hydrogen generation in pure water from the Al–Sn alloys with the four different fractions of Sn after processing by HPT through N = 10. The hydrogen production increases with increasing the Sn fraction. When the Sn fraction is over 40 wt%, the production significantly augments.
Hydrogen generation behavior with time for Al–Sn alloys of four different Sn amounts at room temperature (HPT-processed for N = 10).

Figure 2 illustrates results of the hydrogen generation after processing by HPT through N = 1, 10, and 50 including the one after annealing at 483 K following the HPT processing through N = 10. The solid line represents the theoretical hydrogen production which is 1359 mL/g. It is obvious that the hydrogen production increases when the number of revolution increases from N = 1 to N = 10. However, with the further increase from N = 10 to N = 50, the hydrogen production shows no augmentation but decreases to some extent. The annealing of the HPT-processed sample leads to the lowest hydrogen production. In this study, each of pure Al powders and pure Sn powders were also processed separately by HPT but the hydrogen production is negligible in pure Al and zero in pure Sn. It is therefore inferred that the alloying of Al with Sn and the straining by HPT are important to facilitate hydrogen generation through aluminum hydrolysis reaction.
Hydrogen generation behavior with time for Al–80 wt% Sn alloy at room temperature.
B. Hydrogen generation at higher temperatures
Figure 3 represents results of the hydrogen generation from the Al–80 wt% Sn alloy in pure water at temperatures of 313, 323, and 333 K, respectively after HPT processing for N = 1, 10, and 50. All the samples showed a similar tendency for the hydrogen generation. When compared with the hydrogen generation behavior at room temperature, the generation rate becomes faster during the first few hours and levels off afterward. The generation yield is also greatly raised for all samples at the elevated temperatures but more with the increase in the water temperature. It should be noted that for the sample processed for N = 10, the generation yield becomes close to the theoretical one after one day at 333 K.
Hydrogen generation behavior with time for HPT-processed Al–80 wt% Sn alloy at: (a) 313 K, (b) 323 K, and (c) 333 K.
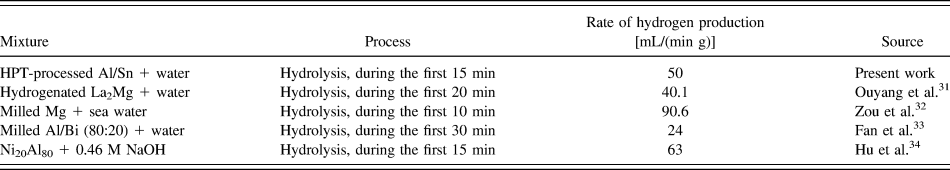
The temperature dependence of hydrogen generation from the Al–80 wt% Sn alloy in pure water after HPT processing for N = 10 is shown in Fig. 4. It is obvious that both the hydrogen generation rate and total production are greatly raised with increase in water temperature. This improvement of hydrogen generation rate at elevated water temperature can be attributed not only to higher hydrogen diffusion through grain boundaries but also to enhanced reaction for hydrogen production. The hydrogen generation rate of the Al–80 wt% Sn alloy at 333 K is about 50 mL/(min g) which is comparable to other materials as documented in Table I.Reference Ouyang, Xu, Dong, Sun and Zhu31−Reference Hu, Qiao, Pei, Fan, Li, Zong and Zhang34
Temperature dependence of hydrogen generation in pure water from HPT-processed Al–80 wt% Sn alloy for N = 10.
Hydrogen production rates for several metal mixtures.
C. XRD profiles
Figure 5 shows XRD profiles of the Al–80 wt% Sn sample processed by HPT through N = 1, 10, and 50 including the annealed sample following N = 10, where (a) and (b) corresponds to the states before and after the hydrogen generation, respectively. The aluminum hydroxide peak [marked by the red rectangular in Fig. 5(b)] appears after the hydrogen generation for all samples but no other peaks except for Al and Sn, indicating that only aluminum reacted with water at room temperature.
XRD profiles for HPT-processed Al–80 wt% Sn alloys: (a) before and (b) after immersion in pure water.
D. Electron probe microanalysis
Figure 6 shows EPMA images of the HPT-processed samples through N = 1, 10, and 50 and the annealed sample after HPT processing for N = 10. For the sample processed through N = 1, the distribution of Sn in the Al matrix is heterogeneous and the interface between Al and Sn is well defined. When N increases from 1 to 10, most part of the image becomes green, thus indicating that the distribution of Sn is more homogeneous at this condition. However, the further increase in N from 10 to 50 gives rise to little improvement in the homogeneity of Sn distribution. Moreover, for the annealed sample, some agglomerations of Sn and Al appeared.
Elemental mapping of Al–80 wt% Sn alloy after HPT processing for (a) N = 1, (b) N = 10, (c) N = 50, and (d) HPT for N = 10 followed by annealing.
E. Electron back scattered diffraction pattern
EBSP results of the HPT-processed samples through N = 1, 10, and 50 are shown in Fig. 7. The sample processed for N = 1 shows a structure consisting of coarse grains with an average grain size of ∼2 μm, while a fine-grained structure with an average grain size of ∼270 nm is found for the sample with N = 10. When N increases further to 50, a structure similar to that of the sample after N = 10 with an average grain size of ∼330 nm is observed except for the appearance of some coarse grains. This grain coarsening can be due to the recovery and recrystallization occurring during HPT processing.
EBSP observation of Al–80 wt% Sn alloy after HPT processing for (a) N = 1, (b) N = 10, and (c) N = 50.
F. TEM observation
Figures 8(a)–8(c) represent TEM bright-field images, dark-field images, and SAED patterns of the HPT-processed samples through N = 1, 10, and 50, respectively. After N = 1, the grain is relatively large as in Fig. 8(a) with an average grain size more than 1 μm. The corresponding SAED pattern does not form rings but shows a net, indicating that the grain refinement was not much attained at this state. With the increasing N from 1 to 10 and 50, the average grain size is reduced to ∼350 and ∼360 nm, respectively. The tendency of the grain size change is in accordance with the one observed by EBSP in Fig. 7. Moreover, ring patterns can be clearly seen in Figs. 8(b) and 8(c) which indicate the formation of ultrafine-grained structures having high-angle boundaries.
TEM micrographs of Al–80 wt% Sn alloy after HPT processing for (a) N = 1, (b) N = 10, and (c) N = 50.
IV. DISCUSSION
The results mentioned above indicate that the addition of Sn in Al and the introduction of lattice defects into the Al alloys through HPT processing significantly influenced the hydrogen generation behavior. The addition of Sn led to the formation of galvanic cells between Al and Sn which enables the hydrolysis of Al in water. An illustration of the Al–Sn galvanic cell is given in Fig. 9, where Al acts as an anode while Sn as a cathode, then hydrogen gas will be released on the interface between Al and Sn. According to an equilibrium phase diagram of the Al–Sn system, the solubility of Sn is very limited in Al and so is the case of Al in Sn at room temperature. It is then likely that the Al/Sn galvanic cell is realized in the Al–Sn alloys.Reference Fan, Sun and Xu35,Reference Hu, Zhu, Zhang, Wang, Gu, Yang, Song, Li, Fang, Jiang and Wang36 In this study, the HPT processing led to a significant grain refinement when the revolution number increased from N = 1 to 10 and therefore increased the density of the Al/Sn interface, which facilitates the hydrolysis reaction. However, with the further increase in the revolution number from N = 10 to 50, grain coarsening occurred due to the recovery and recrystallization as described earlier in Al and Al alloys,Reference Ito and Horita37–Reference Alhamidi, Edalati, Horita, Hirosawa, Matsuda and Terada39 thus reduced the hydrogen production at this state.
Illustration of Al–Sn microgalvanic cell.
Meanwhile, lattice defects like dislocations are also introduced into the Al–Sn alloys during the HPT processing. A part of the energy that results from the HPT processing can be stored as the strain energy in the form of dislocations. Such dislocations as well as the grain boundaries and interfaces provide higher energy to make the alloys thermodynamically unstable and the hydrolysis reaction easier. In the present study, the grain size is refined with the order of N = 1, N = 50, and N = 10, whereas the maximum hydrogen production is enhanced in the corresponding order, indicating that the finer grains yield more hydrogen. However, the energy stored in the dislocations and grain boundaries can be released by annealing at a higher temperature so that less hydrogen is produced. In this study, the Al–Sn alloys annealed at 483 K for 1 h showed a significant decrease in the hydrogen generation.
V. CONCLUSIONS
Appropriate fractions of Sn (more than 60 wt%) and optimal revolutions for HPT processing are required for the Al–Sn powder mixtures to achieve high hydrogen generation rate and yield. The highest generation rate and yield were attained for the HPT-processed Al–80 wt% Sn alloy at 333 K. The homogeneous distribution of Sn in the Al matrix and the defects generated by HPT processing are the main reasons that the HPT-processed sample for N = 10 showed the best hydrogen generation behavior.
ACKNOWLEGEMENTS
We are grateful to Prof. Hiroaki Nakano of Department of Materials Science and Engineering, Kyushu University for useful discussion. One of the authors (Fan Zhang) would like to thank the Ministry of Education, Culture, Sports, Science and Technology (MEXT) of Japan for a Ph.D scholarship. This work was supported in part by the Light Metals Educational Foundation of Japan, in part by the Grant-in-Aids from the MEXT, Japan (Nos. 22102004, 26220909, and 15K14183). The HPT process was carried out in the International Research Center on Giant Straining for Advanced Materials (IRC-GSAM) at Kyushu University.