I. INTRODUCTION
Indium nitride (InN) has attracted considerable attention recently because of its outstanding electrical and optical properties. Among III-nitride semiconductors, InN has the lowest electron effective mass, the highest peak-drift velocity and the highest peak overshoot velocity, which are beneficial for high-electron-mobility transistors (HEMTs).Reference Fu and Chen1,Reference Polyakov and Schwierz2 Moreover, InN has a direct band gap of ∼0.7 eV which enables the III-nitride semiconductors to cover the wave length from deep ultraviolet (AlN, Eg = 6.2 eV) to near infrared (InN, Eg = 0.7 eV).Reference Hurni, Choi, Bierwagen and Speck3,Reference Knuumlbel, Aidam, Cimalla, Kirste, Baeumler, Leancu, Lebedev, Wallauer, Walther and Wagner4 InN has shown great potential in the fields of terahertz emitters,Reference Hwang, Tsai, Lin, Lee, Tsai, Lin, Gwo and Chen5–Reference Wang, Zhao, Zhang, Ishitani, Yoshikawa and Shen8 light-emittingReference Hangleiter9 and photovoltaic applications,Reference Trybus, Namkoong, Henderson, Burnham, Doolittle, Cheung and Cartwright10 etc. In 1972, Hovel and CuomoReference Hovel and Cuomo11 grew InN thin films on sapphire by using radio-frequency sputtering for the first time. With the development of thin film growth technology, researchers have obtained InN thin films using various techniques, such as hydride vapor phase epitaxy (HVPE),Reference Song, Kuryatkov, Basavaraj, Rosenbladt, Nikishin, Holtz, Syrkin, Usikov, Ivantsov and Dmitriev12 metal organic chemical vapor deposition (MOCVD),Reference Rauch, Tuna, Giesen, Heuken and Tuomisto13 radio frequency plasma assisted molecular-beam epitaxy (RF-MBE),Reference Kuyyalil, Tangi and Shivaprasad14 pulsed laser deposition (PLD),Reference Stokker-Cheregi, Nedelcea, Filipescu, Moldovan, Colceag, Ion, Birjega and Dinescu15,Reference Li and Yang16 etc. However, it is still difficult to obtain high-quality InN due to its high equilibrium vapor pressure, low dissociation temperature of nitrogen and the lack of suitable substrates for InN.Reference Huang, Li, Cai and Kang17
To date, sapphire is the most common substrate to grow III-nitride semiconductors. However, InN shares an up to 25% mismatch with sapphire in terms of lattice parameter which results in polycrystalline InN films when directly growing InN on sapphire. A large number of grain boundaries existing in polycrystalline InN films slow down transportation of carriers. As a result, the performance of devices is deteriorated. Consequently, single-crystalline InN films are highly desired. If sapphire substrates are nitrided before the growth of InN films, a thin nitrided layer might be formed on the sapphire surface. This nitrided layer, i.e., AlN interlayer, can act as a buffer between sapphire and InN. As pointed out, InN shares a lattice mismatch of 25% and 13.9% with sapphire and AlN, respectively. Therefore, the generation of an AlN interlayer on the surface of a sapphire substrate dramatically decreases the lattice mismatch between InN and sapphire. Meanwhile, it should be noted that In atoms have strong adhesion on sapphire substrates, which results in low lateral migration and accumulation of In atoms on the sapphire surface, leading to a rough surface of the as-grown InN film. The formation of an AlN interlayer on the other hand prohibits the accumulation of In atoms on the sapphire surface, so as to provide a smooth surface and a good template for the succeeding InN epitaxial growth, which plays an important role in improving the film quality of the as-grown InN film on sapphire. In this paper, we focus on the influence of sapphire nitridation on the formation of a nitrided interlayer, as well as its impact on the as-grown InN film quality, and consequently propose an optimal nitridation condition and its corresponding interlayer state for high-quality InN films grown on sapphire substrates.
II. EXPERIMENTAL
InN films were grown by RF-MBE on (0001) sapphire substrates. High purity indium (7N) and nitrogen gas (7N) were used as the sources, respectively. Sapphire substrates were degreased by organic solvents, etched in a hot solution of H2SO4 and H3PO4 (H2SO4:H3PO4 = 3:1) at 160 °C for 30 min, rinsed with deionized water, and finally dried by 7N nitrogen before being put into the MBE load-lock chamber with pressure 1 × 10⁻⁷ Torr. The substrates were then transferred into the high vacuum MBE growth chamber at pressure 1.0 × 10⁻¹⁰ Torr, and thermally cleaned at 800 °C for 30 min to remove residual surface contaminations. Before InN growth, the nitridation of sapphire was carried out at 550 °C with a nitrogen flow rate of 1 sccm and a RF plasma power of 240 W. Subsequently, a low-temperature InN buffer layer was grown at 350 °C for 5 min with a nitrogen flow rate of 2 sccm and a RF plasma power of 400 W. In the end, a high-temperature InN layer was grown at 550 °C for 60 min with a nitrogen flow rate of 2 sccm and a RF plasma power of 240 W. A quartz crystal microbalance (QCM) was used to monitor the deposition rate during the growth. It reveals that the thicknesses for the low- and the high-temperature InN layers are 10 and 200 nm, respectively. The as-grown InN films were evaluated by x-ray diffraction (XRD, with Cu Kα1 as an x-ray source) for crystallinity by Bruker D8 Discover. Cross-sectional high resolution transmission electron microscopy (HRTEM) was carried out to study the interfaces between the substrates and InN films. The HRTEM samples were put into a JEOL 3000F field emission gun TEM (Tokyo, Japan) working at a voltage of 300 kV, which gives a point to point resolution of 0.17 nm. Electron energy loss spectroscopy (EELS) collections were carried out under scanning TEM mode, where a spot formed by a 0.6 nm diameter electron beam was used to scan across the interface with an interval of 1 nm between two spots. Scanning electron microscopy (SEM) was then carried out to evaluate the microstructure of InN films by FEI Nova NanoSEM 430 (Hillsboro, OR). Hall effect measurements were also performed at room temperature to obtain carrier characteristics with a 3000 Gauss magnet.
III. RESULTS AND DISCUSSION
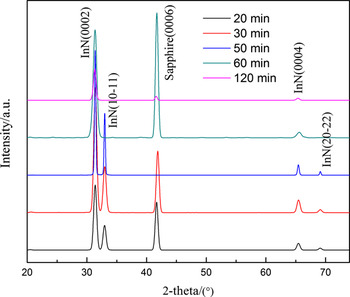
Figure 1 shows the XRD patterns for InN films grown on (0001) sapphire nitrided with different durations of 20, 30, 50, 60, and 120 min, respectively. Peaks located at 31.02 and 64.66° are from hexagonal InN (0002) and (0004) planes, those at 33.0 and 69.22° are from InN (10-11) and (20-22) planes, and the one at 41.6° is from sapphire (0006) plane. Apparently, InN films grown on sapphire substrates with nitridation durations of 20, 30, and 50 min are polycrystalline with two growth directions of <0001> (c axis) and <10-11>, while InN films grown on sapphire substrates with nitridation durations of 60 and 120 min are single-crystalline with c axis as the growth direction. This indicates that the nitridation duration of the sapphire substrate plays a critical role in determining the crystalline form and the growth direction of as-grown InN films. Too short nitridation duration of sapphire substrates leads to polycrystalline InN films, while a nitridation duration of longer than 60 min helps to obtain single-crystalline InN films on sapphire substrates.
XRD patterns of the InN films grown on (0001) sapphire substrates with various nitridation durations.

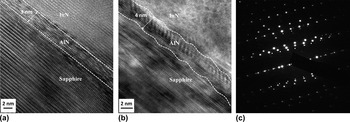
To better understand this finding, HRTEM is carried out to study the interface between the sapphire substrate and the InN epitaxial film. Figure 2(a) is the HRTEM image for an InN sample with 60 min nitridation. One can clearly notice a continuous interlayer with the thickness of ∼3 nm between the sapphire substrate and the InN epitaxial film. This continuous interlayer is very flat and ordered, as illustrated by the two parallel dotted lines in Fig. 2(a). The concentration of this interlayer has also been characterized by EELS attached to this TEM. It reveals that only Al and N are contained in this interlayer, and no trace of O is detected. EELS measurement further reveals that the atomic ratio between Al and N is 1, or equally, AlN. It suggests that the following reaction take places when sapphire substrates are nitrided by N plasma at high temperature,
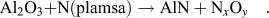 $${\rm{Al}}_{\rm{2}} {\rm{O}}_{\rm{3}} {\rm{ + N(plamsa)}} \to {\rm{AlN + N}}_x {\rm{O}}_y \quad.$$
(a) Cross-sectional HRTEM images around the interface between the sapphire substrate and the InN film with (a) 60 min and (b) 120 min nitridations, and (c) the corresponding selected area electron diffraction pattern of (a), where 3 groups of patterns could be spotted.

The newly generated NxOy is in the gaseous state and will be exhausted by the MBE pumping system, leaving a fresh AlN surface on the sapphire substrate. Selected area electron diffraction around this interface by TEM is given in Fig. 2(c). Careful investigation lets us to spot three groups of diffractions, from sapphire, AlN, and InN, respectively. It once again confirms the existence of the AlN interlayer.
Interestingly, further increase in nitridation duration will lead to a poorer-quality interlayer, as shown in Fig. 2(b), the cross-sectional HRTEM image of an InN sample with 120 min nitridation. The thickness of the interlayer with 120 min nitridation is ∼4 nm, which is only slightly thicker, other than 2 times thicker considering the nitridation duration, than that after 60 min nitridation. It suggests that after a continuous AlN interlayer is formed following 60 min nitridation, it becomes much more difficult for N plasma to diffuse and penetrate the interlayer and react with the internal sapphire. More important information we get from Fig. 2(b) is that the interlayer with 120 min nitridation becomes very wavy and rough, and also much more stressed and disordered when compared with the straight and smooth interlayer surface with 60 min nitridation. This wavy and rough AlN interlayer undoubtably has a negative impact on the surface migration of In atoms on the substrate surface, which deteriorates the quality of the subsequently grown InN film that has been verified by our Hall effect measurement of the samples as discussed later. TEM findings suggest that too long exposure to the highly energetic N plasma will damage the surface of the interlayer and hence the as-grown InN film quality, which is consistent with our SEM observation.
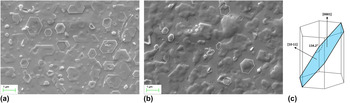
The surface morphology of the as-grown InN films is characterized by SEM. Figures 3(a) and 3(b) show those with nitridation duration of 20 and 30 min, respectively. We note that both samples share a similarly rough morphology. Apart from those coalesced or overlapped grains, we can also clearly notice two types of grains with different shapes, as representatively stand out in the images. Bear in mind that XRD measurement has revealed that both the films will have two growth directions, i.e., <0001> and <10-11>. As a reference, we schematically illustrate these two growth directions and their corresponding planes in the InN’s wurtzite structure, Fig. 3(c), only to find out the shapes of the two types of grains match perfectly with the {0001} and {10-11} planes, respectively. We can then deduce that those of regular hexagonal shapes are from InN grown along the <0001> direction, and those of irregular hexagonal shapes are from InN grown along the <10-11> direction. The sizes of two types of grains are within the same range, from ∼0.5 to 1.0 μm, and the proportion of the two types of grains are almost the same. A further increase in nitridation duration of the sapphire substrates up to 50 min will not change the surface morphologies of InN films, which has been confirmed by SEM observation. Obviously, under this polycrystalline growth condition with nitridation duration no longer than 50 min, the two types of grains share the same growth opportunity and no one will prevail over the other.
SEM images of InN films grown on sapphire substrates nitrided for (a) 20 min and (b) 30 min, respectively, and (c) the schematic illustration of a InN’s wurtzite structure as well as its two growth directions of <0001> and <10-11>.

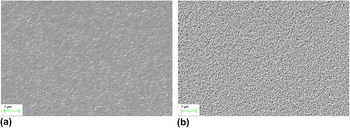
Figure 4(a) shows the SEM image of an InN film grown on a sapphire substrate nitrided for 60 min. Different from InN films with less than 50 min nitridation, this film contains grains only of <0001> growth direction. These grains coalesce to each other very well, leading to a much flatter surface than those polycrystalline films. Figure 4(b) shows the SEM image of an InN film grown on a sapphire substrate nitrided for 120 min. Surprisingly, this film exhibits much smaller uncoalesced grains and a much rougher surface when compared with the InN film nitrided for 60 min, although both films are single-crystalline. Obviously, a too long nitridation duration actually damages the film quality of the as-grown InN film.
SEM images of InN films grown on sapphire substrates nitrided for (a) 60 min and (b) 120 min.

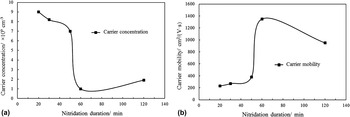
Room-temperature Hall effect measurement has been carried out with a 3000 Gauss magnet to characterize the carrier transportation properties of the as-grown InN films. For this purpose, samples were cut into 10 × 10 mm2 and In foil was pressed on to form the van der Pauw configuration with Ohmic contacts. As we know, InN has a very large electron affinity.Reference Lu, Schaff, Eastman and Stutz18–Reference Mahboob, Veal, McConville, Lu and Schaff20 Therefore, it is not surprising that all of our as-grown undoped InN films exhibit n-type conductivity, due to the pinning of the Fermi level above the conduction band edge. Figure 5(a) shows the carrier concentration for the as-grown samples as a function of nitridation duration. We find that polycrystalline InN films have much higher carrier concentration than single-crystalline InN, which we attribute to the defects in polycrystalline films due to the poor surface migration of In atoms on sapphire substrates.Reference Bhuiyan, Hashimoto and Yamamoto21 Among polycrystalline InN samples with nitridation duration no longer than 50 min, the increment in nitridation duration slightly decreases the carrier concentration, implying some more AlN islands formed on sapphire substrates which enhances the surface migration of In atoms and hence the film quality. A steep drop in carrier concentration takes place at 60 min nitridation, from 5.5 × 10¹⁹ to 1.0 × 1019 cm−3, which indicates a very high quality InN film. This is because of the formation of the continuous AlN interlayer, and consequently the dramatically improved surface migration of In atoms on the substrate. However, a further increment in nitridation duration will raise the carrier concentration, Fig. 5(a), from 1.0 × 10¹⁹ to 1.9 × 1019 cm−3, indicating a worsen InN film quality. As discussed above, we attribute this to the roughened surface of the AlN interlayer due to too long bombarding by highly energetic N plasma, which decreases In atom surface migration.
Room-temperature Hall effect measurement of as-grown InN films with various nitridation durations. (a) Carrier concentration, and (b) carrier mobility.

Figure 5(b) shows the carrier mobility for the as-grown samples as a function of nitridation duration. The as-grown InN films grown with nitridation durations of 20, 30, 50, 60, and 120 min have a carrier mobility of 230, 270, 380, 1350, and 950 cm2/(V·s), respectively. Similar to what happens to the carrier concentration, polycrystalline InN samples with nitridation duration no longer than 50 min show very poor carrier mobility of less than 400 cm2/(V·s), and single-crystalline InN samples with 60 min nitridation show very high film quality with carrier mobility up to 1350 cm2/(V·s). Likewise, further increases in nitridation duration up to 120 min will damage the AlN interlayer quality, which appears as a diminishing carrier mobility of 950 cm2/(V·s). The results from Hall effect measurement once again confirm the importance of an optimal nitridation duration of sapphire substrates to the as-grown InN film quality. In other words, 60 min nitridation brings up with a smooth and ordered AlN interlayer on top of sapphire which improves the surface migration of In atoms in InN films, and consequently enhances carrier properties.
It is not hard to understand that there is an optimal value for the nitridation duration. Too short nitridation duration will be not enough to form a continuous AlN layer on the sapphire surface, and a proportion of sapphire surface is still exposed to In atoms during the growth where In atoms will unavoidably accumulate. Under such a circumstance, as-grown InN films will be polycrystalline with a rough surface. On the contrary, if nitridation duration is long enough (up to 60 min), a continuous AlN interlayer can fully cover the sapphire surface. In atoms obtain much better migration ability on AlN. Moreover, InN shares much smaller in-plane lattice mismatch with AlN. The epitaxial growth condition along c axis for the InN film has therefore been achieved. Accordingly, a single-crystalline InN film is grown. If a nitridation duration longer than 60 min is applied to sapphire substrates, the newly formed continuous AlN interlayer will be enduring too long bombarding by the highly energetic N plasma which damages the surface of the interlayer, resulting in a decrease in InN film quality.
IV. CONCLUSIONS
InN films have been grown on sapphire substrates nitrided with different durations by RF-MBE. It is found that nitridation duration of the sapphire substrates determines the as-grown film quality. Nitridation duration of no longer than 50 min will end up with a polycrystalline InN film with two growth directions of <0001> and <10-11>, while nitridation duration of 60 min will bring up with a single-crystalline c-plane InN film of high quality with 1.0 × 1019 cm−3 carrier density and 1350 cm2/(V·s) carrier mobility. However, a further increment in nitridation duration will worsen the as-grown quality though it is still single-crystalline.
EELS analysis on the interlayer between the InN film and the nitrided sapphire substrate by cross-sectional HRTEM reveal that AlN is generated on the sapphire surface during the nitridation by N plasma, and 60 min nitridation leads to a continuously straight and smooth AlN interlayer of ∼3 nm which enormously enhances the surface migration of In atoms on the substrate, resulting in a high-quality single-crystalline InN film with excellent carrier properties. Too short nitridation duration of no more than 50 min will be not enough to form a continuous AlN layer on the sapphire surface, and a proportion of the sapphire surface is still exposed to In atoms during the growth where In atoms will unavoidably accumulate. That’s the reason why a polycrystalline InN film is obtained. On the other hand, if a nitridation duration of longer than 60 min is applied to sapphire substrates, the newly formed continuous AlN interlayer will be enduring too long bombarding by the highly energetic N plasma which damages the surface of the interlayer, resulting in a decrease in InN film quality.
To conclude, it is the right optimal nitridation duration that helps to form an ordered and flat AlN interlayer between the substrate and the InN film, which improves the surface migration on In atoms on the substrate, and consequently helps to obtain a high-quality InN film.
ACKNOWLEDGMENTS
This work is supported by National Science Foundation of China (Contract No. 51002052), and Key Project in Science and Technology of Guangdong Province (Contract No. 2011A080801018).